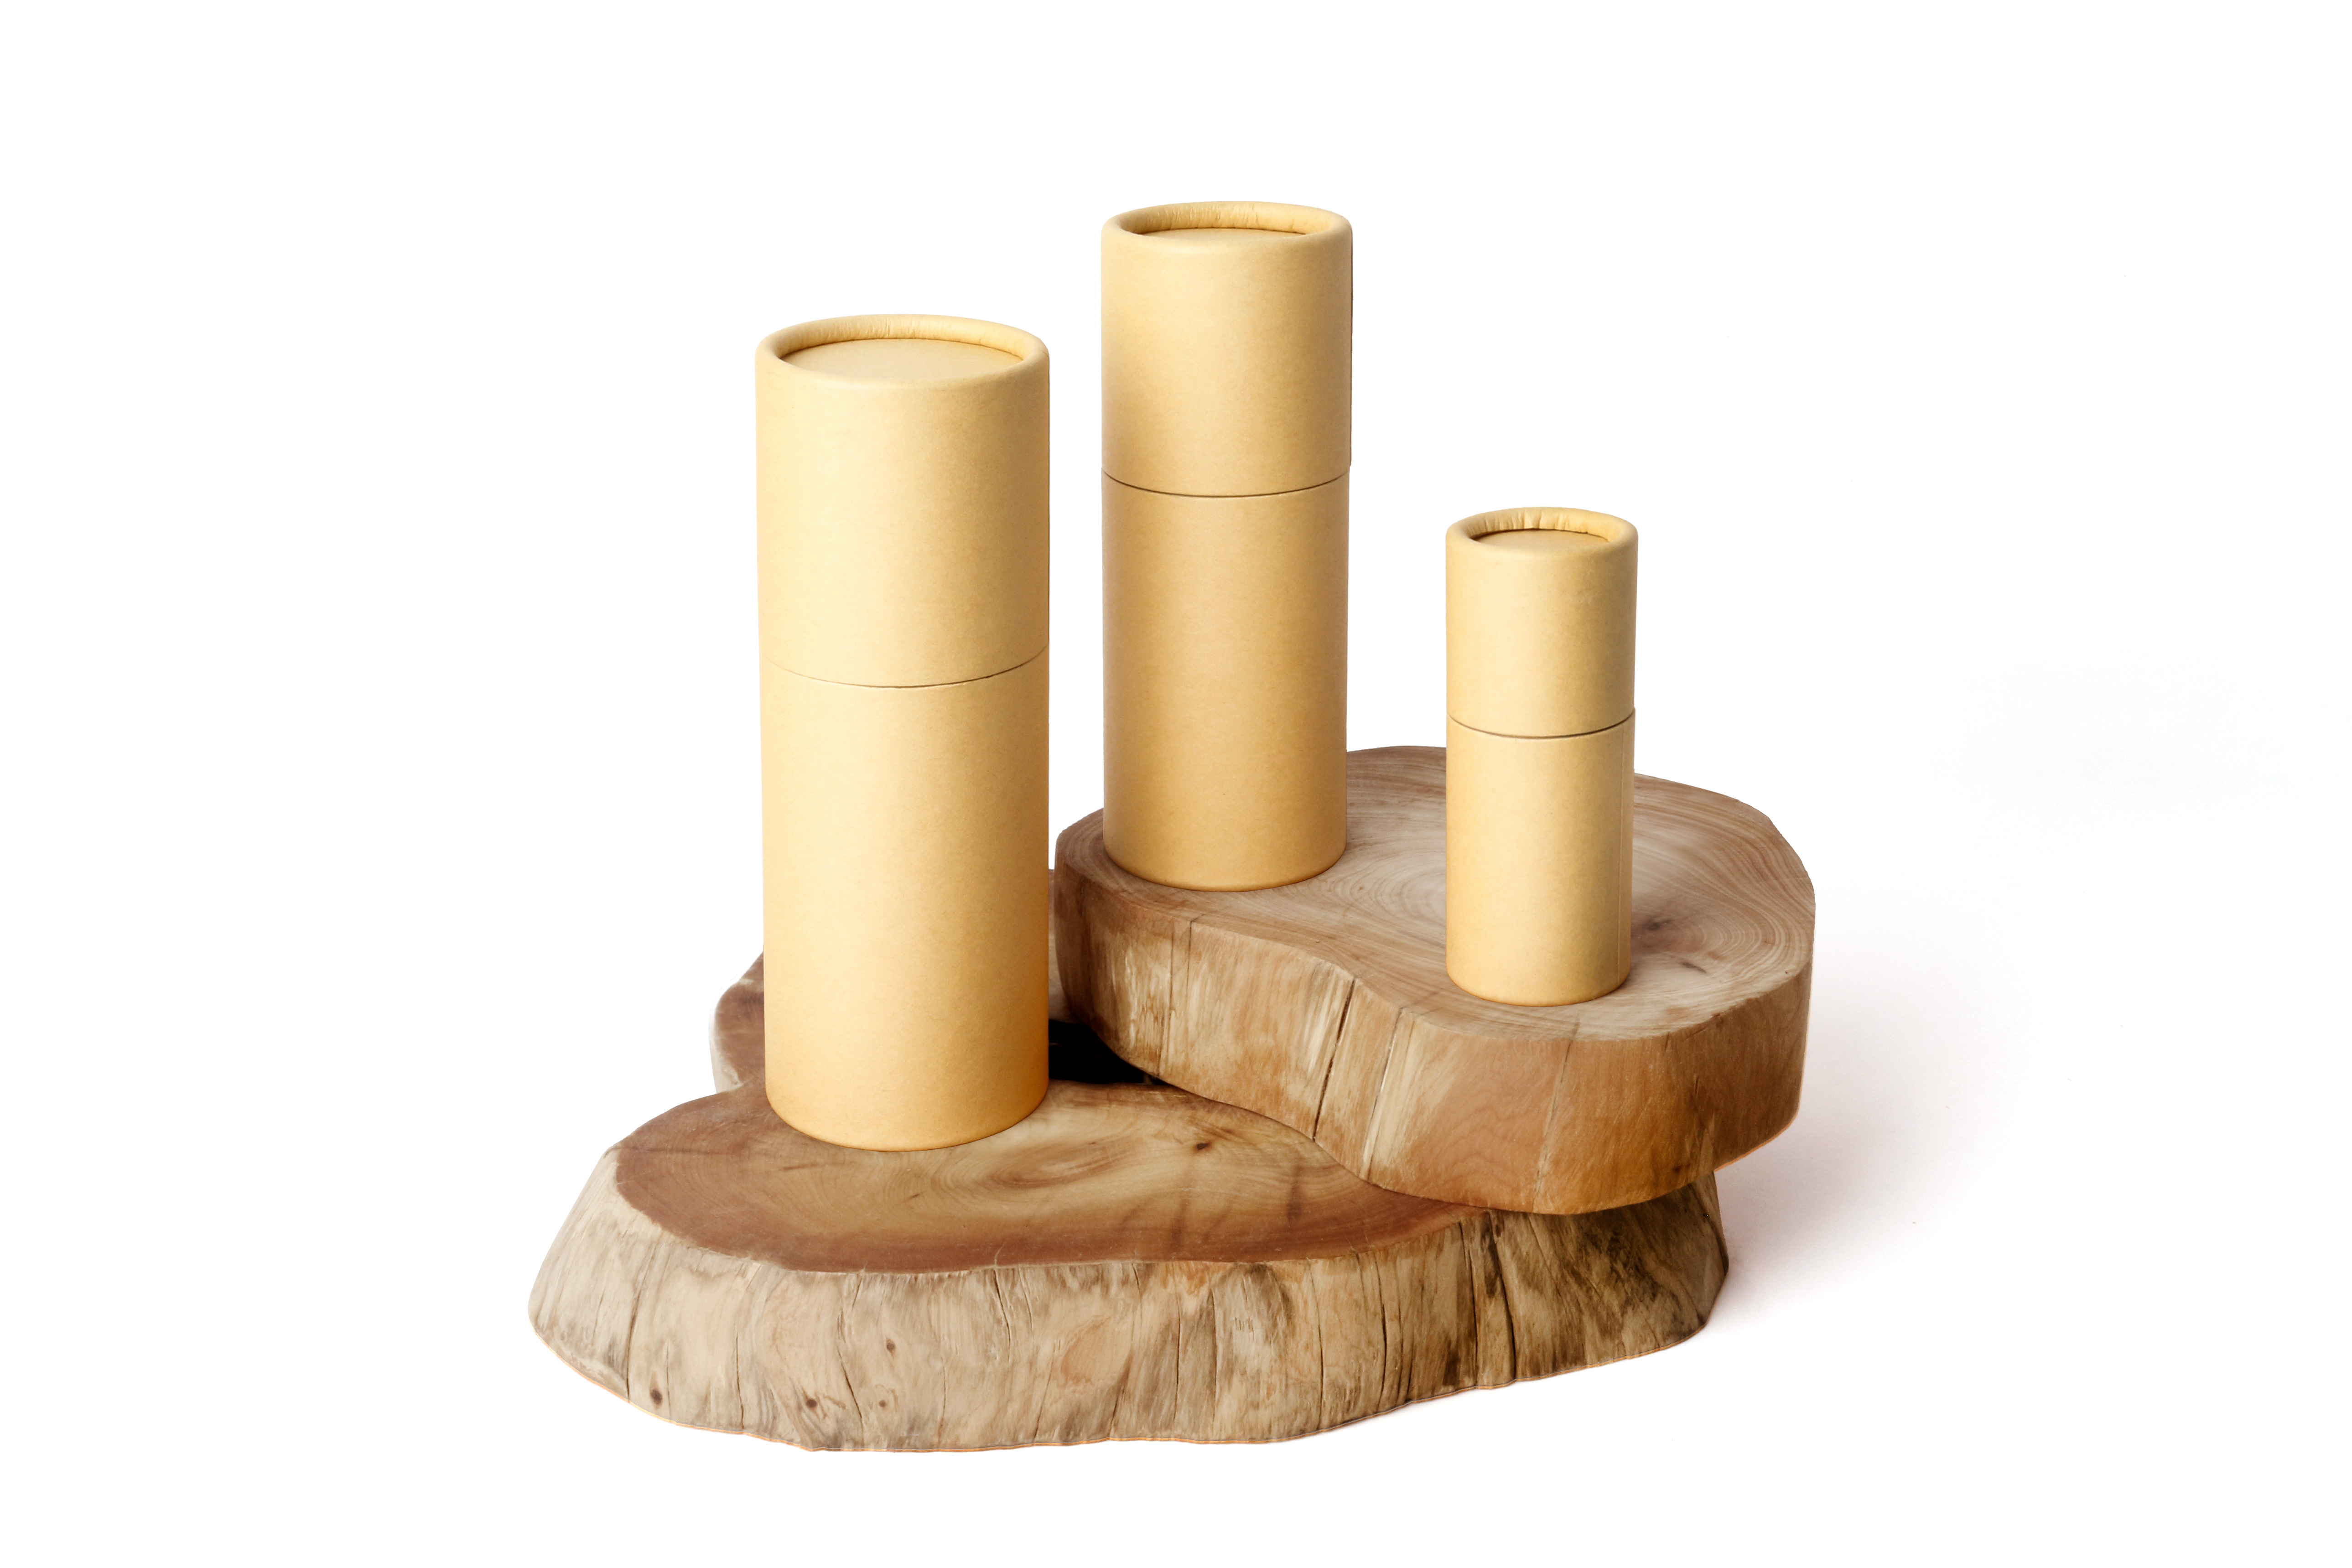
Wall thickness is the one number buyers most often ask for and the one number most often specified badly. A tube wall is not chosen from a catalogue; it is the result of how many paper plies are wound, how heavy each ply is, and how tightly they are bonded. That wall then decides three things at once — how much load the tube carries, how the lid fits, and what the unit costs. If you specify only a thickness figure, you are specifying an output and skipping the inputs that actually control it. Specify the job the wall has to do, and let the construction follow.
Why “Thicker Is Better” Is the Wrong Starting Point
When a tube feels flimsy, the instinct is to add wall. Sometimes that is right; often it is an expensive way to solve the wrong problem, because thickness sits where three requirements meet and raising it helps one while hurting another.
It buys strength, at a material cost. A thicker wall resists axial compression and side crush better, so it stacks higher in a warehouse and survives rougher handling. It also uses more paper per tube and takes longer to wind, and both of those land in your unit price. Paying for strength the product does not need is one of the most common silent overspends in packaging.
It changes the fit, and not always for the better. Wall thickness moves the outer diameter if the inner diameter is held, or the inner diameter if the outer is held. Change the wall without changing the lid, and you have changed the interference between the two parts. A wall upgrade that was meant to fix crush damage can quietly turn a snug lid into a loose one.
It narrows the process window. Heavier plies are stiffer and harder to wind consistently around a small diameter. On tight radii, an aggressive wall can produce seam marking, ovality, or a rougher cut edge — which then shows up in print and in how the lid seats.
The practical consequence: wall thickness should be the last thing you fix, not the first.
How a Wound Paper Tube Actually Gets Its Wall
A paper tube wall is built, not moulded. Understanding the build explains why thickness tolerances behave differently from plastic or metal.
Plies. The wall is a stack of paper layers bonded with adhesive. Total thickness is roughly the sum of the ply calipers plus the adhesive lines between them. Adding a ply changes the wall more than switching to a slightly heavier grade of the same ply count, and the two routes are not interchangeable in terms of stiffness.
Winding direction. Spiral winding runs the paper at an angle, which spreads the seam around the tube and suits long production runs. Convolute winding wraps the paper parallel to the axis, producing a wall with different seam behaviour and a different feel in the hand. They do not deliver the same stiffness at the same nominal thickness, which is why comparing two quotes on a thickness figure alone is unreliable.
Adhesive and tension. The bond line contributes thickness and the winding tension decides how much the plies compress. A wall wound loose measures close to nominal but behaves softer under load, because the layers can move against each other.
Cutting and finishing. The cut edge is where buyers actually see the wall. A clean, square cut exposes an even ply stack; a ragged cut makes the tube look thinner than it is and interferes with how the lid sits.
The Four Jobs the Wall Has to Do
Rather than arguing about a number, describe what the wall must survive. These are the four jobs we ask buyers to rank.
Carry load in the stack. Tubes are usually stored and shipped upright, so the wall carries the weight of everything above it plus its own contents. The relevant questions are how tall the pallet stack gets, how long it stays stacked, and whether it crosses a humid sea leg where paper softens. A tube that holds perfectly in a dry warehouse can creep under the same load after two weeks in a container.
Resist side crush. This is the job that matters once the carton is being handled, dropped, or compressed by other freight. Radial stiffness comes mainly from the wall build and the diameter; small diameters are inherently stiffer, which is why a slim lip balm tube feels solid at a wall that would feel thin on a wide canister.
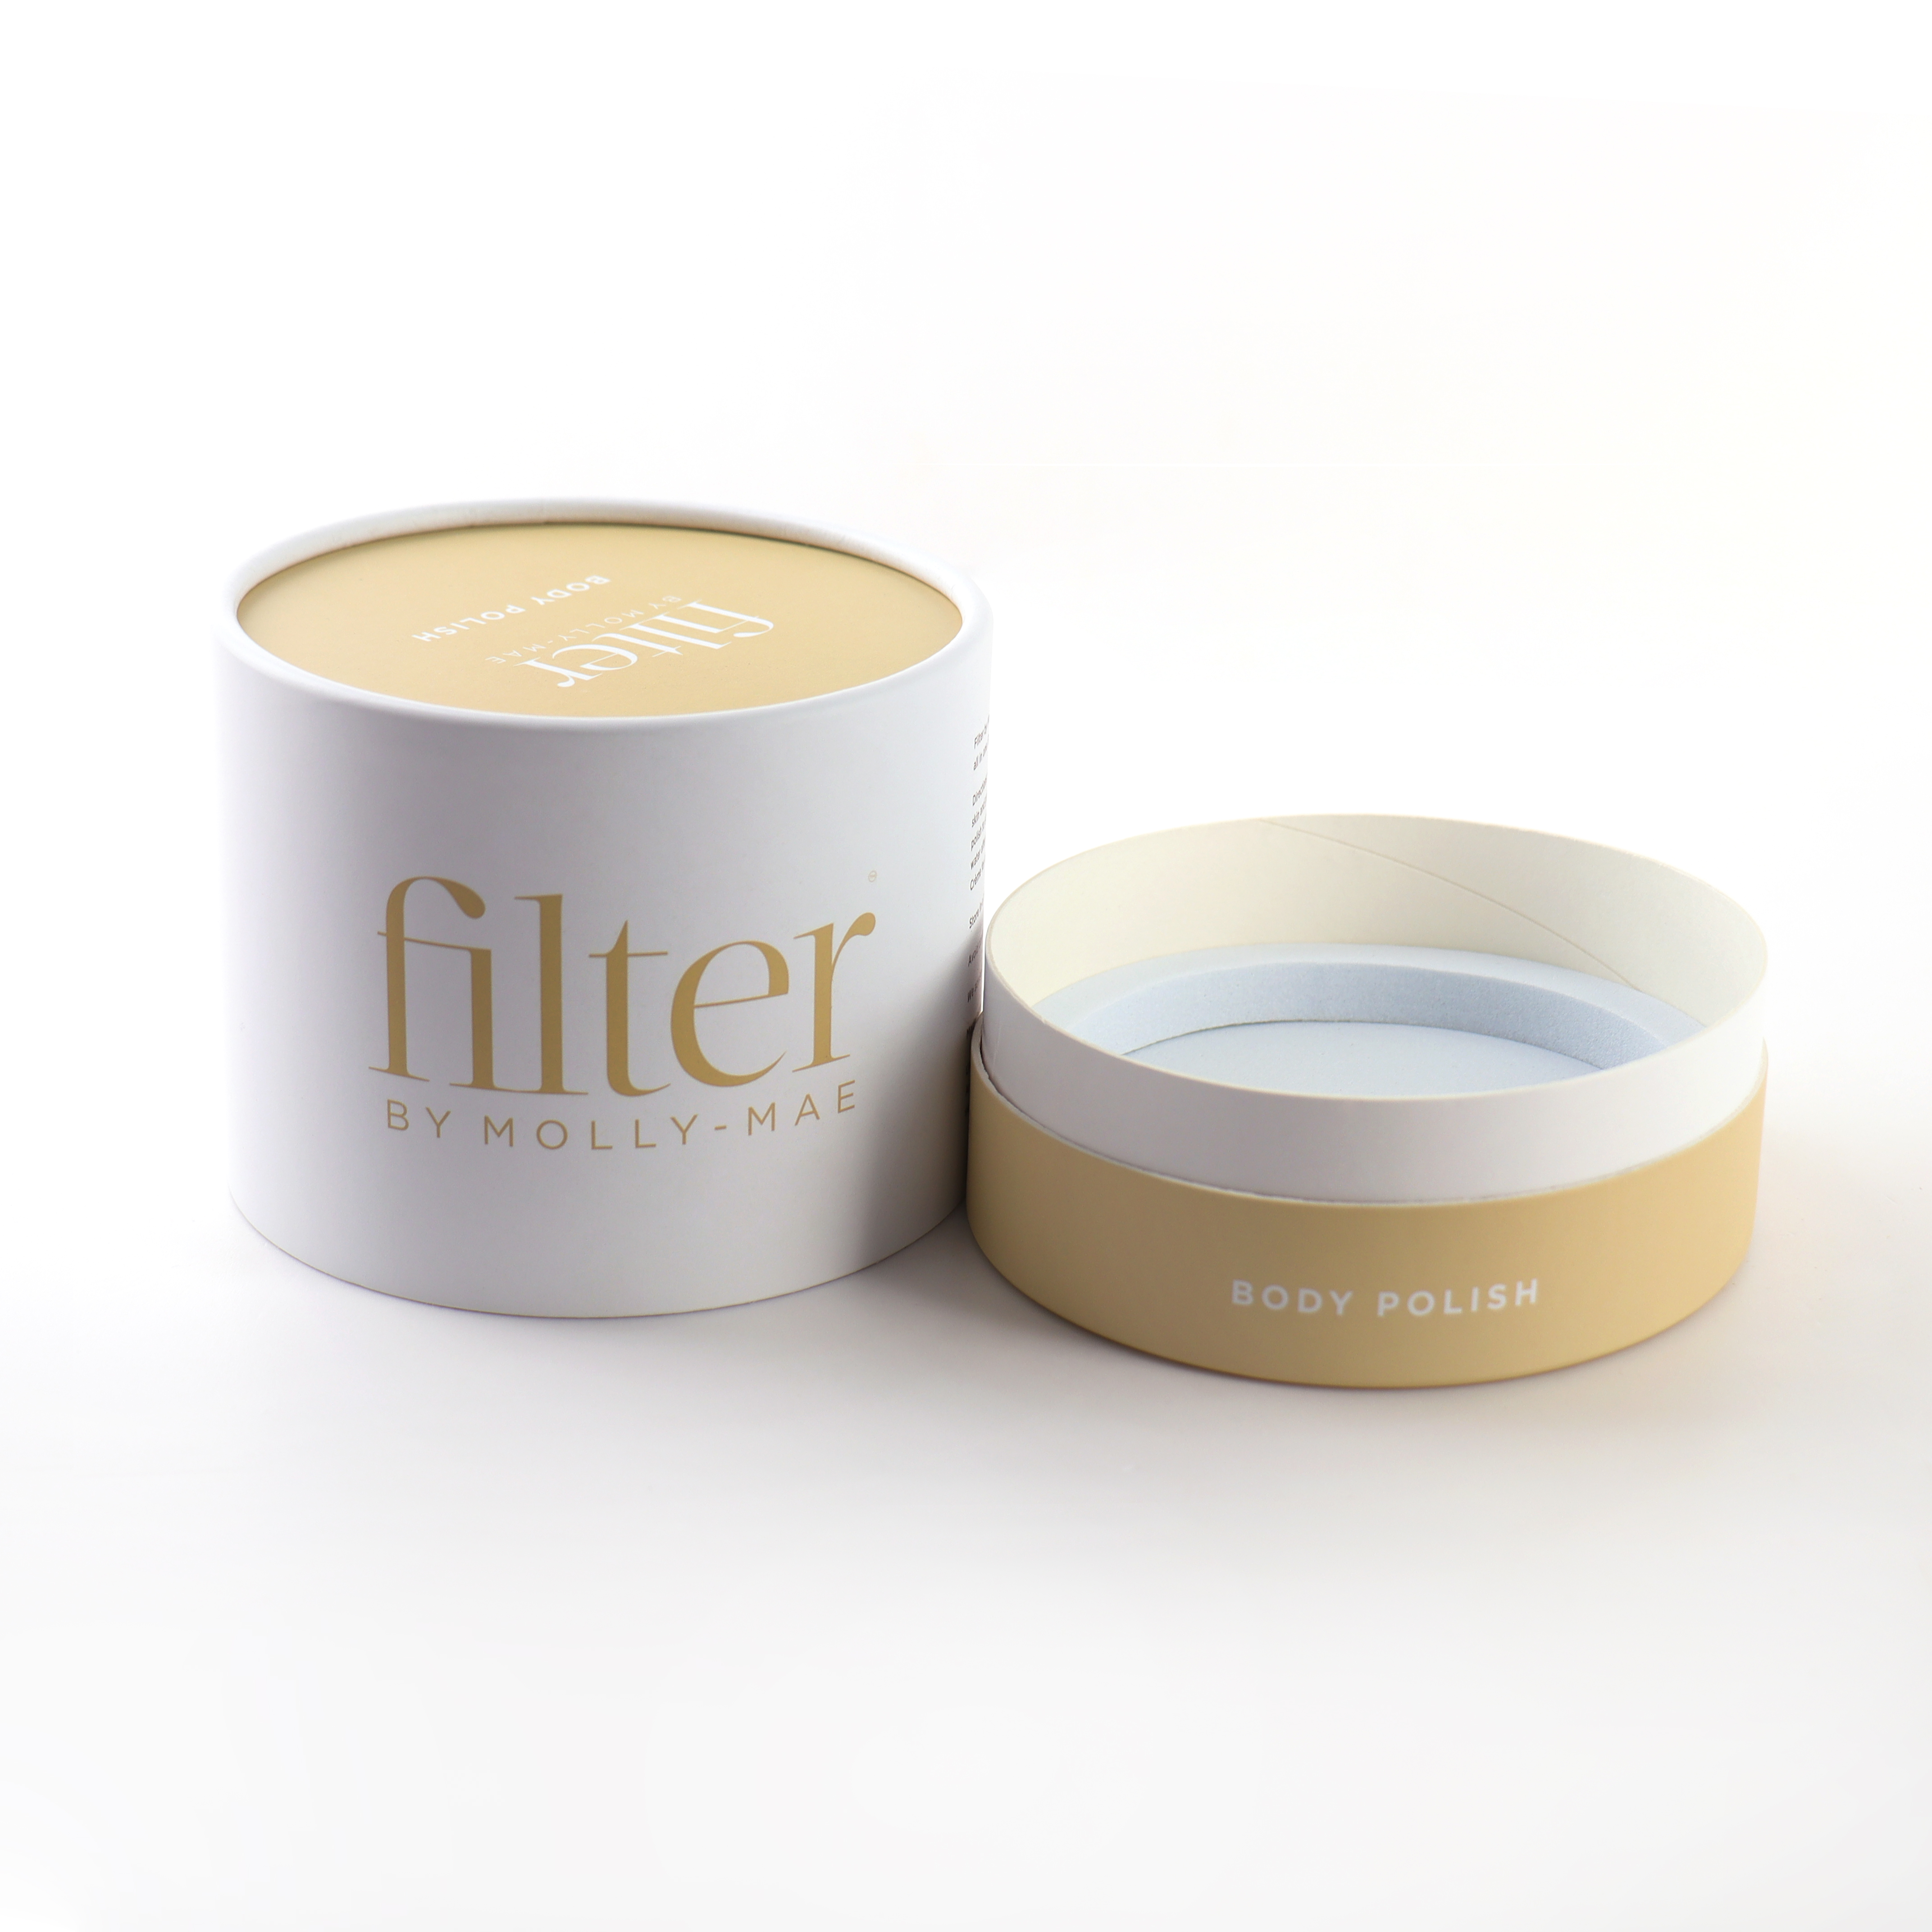
Hold the closure. The lid grips the outside of the body, so the outer surface and its roundness matter as much as the wall. Ovality — a tube slightly out of round — creates tight and loose zones around the same lid, which is one reason a lid can feel inconsistent with no single dimension out of tolerance.
Accept decoration. Embossing and debossing need material to displace. On a thin or loosely wound wall, a deep emboss can telegraph through to the inside, mark the product, or simply not hold its definition. Foil and spot UV care less about thickness, but they do care about surface smoothness, which is a function of how evenly the plies were laid.
| Job | What actually drives it | Failure you will see |
|---|---|---|
| Stack load | Ply count, bond quality, moisture content | Bottom tubes ovalise or buckle |
| Side crush | Wall build and tube diameter | Dents, creases, cracked print |
| Lid grip | Outer diameter, roundness, surface | Lid loose in one direction only |
| Decoration | Surface density and smoothness | Emboss fades or shows inside |
The Fit Equation: Wall, Diameter and Lid Together
Buyers often treat wall thickness and lid fit as separate specifications, but they are the same specification seen from two sides. Once the inner diameter is fixed by the product, the wall sets the outer diameter, and the lid has to be sized against that outer diameter.
This is why late wall changes are so disruptive. Increasing the wall to solve crush damage grows the outer diameter; if the lid drawing is not revised, the lid becomes tight, and any sanding fix varies from batch to batch. Decreasing the wall to save cost produces the opposite complaint.
The safe sequence is: fix the product cavity, choose the closure family, then size the wall so that both the inner cavity and the outer fit land where they need to. Our closure selection guide covers how each closure type engages the body, and it is worth reading before the wall is locked.
Where Thickness Varies in Real Production
A wall that measures correctly on a sample can drift during a run. These are the sources we watch.
Paper caliper tolerance. Paperboard is sold to a caliper range, not an exact figure. A new pallet of the same grade can sit at a different point in that range, shifting the finished wall without any change to the winding setup.
Adhesive laydown. Glue lines add measurable thickness. A slightly heavier laydown increases wall and can also stiffen the tube, so the change is not purely dimensional.
Winding tension. Tension compresses the plies. Consistent tension gives a consistent wall; drifting tension gives a wall that varies along the length of the same tube, which is hard to catch with a single measurement at the end.
Moisture. Paperboard picks up moisture from the air. A humid spell changes caliper and stiffness, so measurements from different seasons are not strictly comparable unless conditions are noted.
Tooling condition. Mandrels and forming belts wear. Wear shows up first as ovality and seam inconsistency rather than as a thickness change, which is why thickness alone is a poor inspection metric.
Five Checks You Can Run on a Sample Desk
You do not need a lab to find an under-built tube. These checks take a few minutes and tell you more than a datasheet.
Squeeze test. Hold the tube horizontally and squeeze gently at mid-height. It should flex and recover without a crease. A permanent crease means the wall or the bond is too soft for handling.
Stack test. Load four or five filled tubes on top of one and leave them a day at room temperature. Measure the bottom tube before and after; visible shortening is the early warning for a warehouse problem.
Rim inspection. Look straight at the cut edge. You should see an even band of plies with no delamination and no crushed zone. Gaps between plies are a bond problem, not a thickness problem, and they will worsen with moisture.
Roundness check. Rotate the lid through a full turn on the tube. If resistance changes noticeably at certain angles, the body is oval rather than uniformly undersized — a different fix entirely.
Weight per unit. Weigh ten tubes of the same size and compare the spread. Wide spread points to inconsistent ply build or moisture, even when the wall measures on target.
How to Write the Wall Spec Into an RFQ
A wall specification that only says “1.5 mm” invites a quote you cannot compare. A specification that describes the duty invites a quote you can. Here is what we ask buyers to include.
Product weight and fill. The single most useful number. A 30 g lip balm and a 500 g candle in the same diameter need completely different walls.
Stack height and duration. How many units per carton, how many cartons per pallet, and how long the pallet sits. Two weeks in a dry warehouse and eight weeks in a humid one are different engineering problems.
Closure type and target feel. State the closure family and the fit expectation, so the wall is sized together with the lid rather than before it.
Decorative processes. Deep emboss, deboss and heavy texture need wall margin. Say so up front instead of discovering it at proof stage.
Target wall with a tolerance and a test method. If you must name a figure, name the range and how it will be measured — at the cut edge, at mid-height, at how many points around the circumference. A number without a method is not a specification.
If you are building this specification from scratch, our supplier guide sets out what a well-prepared brief should contain before a factory can quote accurately.
Structure Choices That Change the Wall Question
The structure you pick determines how much of the wall's job is stiffness and how much is fit.
A one-piece tube uses the body wall for everything: stack load, crush, and both end closures. It is the simplest to control and the most dependent on getting the wall right, because there is no second part to absorb variation.
A two-piece telescopic tube adds a lid that slides over the body, so the body's outer wall is now also a bearing surface. Wall consistency around the circumference matters more here than raw thickness, because the lid samples every point of that circumference as it turns.
A three-piece butt-joint tube seats the lid on a shoulder, which is more forgiving of slight wall variation and generally more resistant to rattle. The trade-off is that the shoulder has to be formed consistently, so the critical dimension moves from the cylindrical wall to the joint.
The Cost Side, Honestly
Wall thickness is one of the clearest cost drivers in a paper tube, and it is worth understanding where the money goes before you negotiate.
More plies means more paper and adhesive per tube, slower winding, and more machine time per unit. It also adds weight to the shipping carton, which raises freight on every unit you export — on a long sea leg the freight penalty can approach the material saving. Matching the wall to the job is a commercial decision, not only a technical one.
The reverse trade-off is real too. A wall that is too light saves money at quotation and loses it later in crushed stock, customer complaints, and replacement shipments. Our pricing guide explains how construction choices flow into the quote, and it is the honest place to see what a wall change is likely to do to your unit cost.
How We Set Wall Thickness With a Buyer
Our process starts from the product and the journey, not a stock wall. Once dimensions are confirmed we issue the dieline, and the wall is agreed on that drawing so cavity, outer diameter and closure are fixed together. If the product is heavy, stacked high, or shipping through a humid corridor, we say so at this stage rather than discovering it at the complaint stage.
Sampling then tests the decision in the hand: stock samples are free, while a custom printed sample is built to your specification and carries a sampling charge. Production runs under our ISO-standard quality control, using FSC® certified paper and soy ink printing, typically two to three weeks after sample approval. The full workflow and document set are on our FAQ and certifications page.
If you are still deciding which structure you need, our product type overview shows the three formats side by side, and our design guide covers the decisions that should be settled before the wall is chosen.
Frequently Asked Questions
Is a thicker wall always stronger?
Not always. Bond quality and winding tension matter as much as thickness; a loosely wound thick wall can perform worse than a well-bonded thinner one.
Will a thicker wall change my lid fit?
Yes, if the inner diameter is held. The outer diameter grows with the wall, so the lid must be resized at the same time.
How do I measure wall thickness correctly?
Measure at the cut edge with a caliper at several points around the circumference. Single-point readings hide ovality.
Does wall thickness affect printing quality?
Indirectly. A smooth, evenly wound surface prints and embosses more cleanly, and a wall with enough substance holds emboss definition without marking the inside.
Can I reduce the wall to cut cost?
Only against a defined duty. If you know the stack height, product weight and transit conditions, a lighter wall is often safe and cheaper.
Why does the same spec feel different between orders?
Caliper batch, adhesive laydown, tension and moisture all move the finished wall. Ask for first-article checks each run.
Not Sure How Thick Your Tube Needs to Be?
Tell us the product weight, stack height and closure type. We will recommend a wall construction and send samples so you can feel it before committing.
Request a Quote